Electrical Engineering

What is an Electrical Isolator : Working & Its Applications

 What is an Electrical Isolator : Working & Its Applications:-

The isolator is one type of switching device, and the main function of this is to make sure that a circuit is totally not triggered in order to perform the preservation. These are also recognizable like isolation switches to isolate the circuits. These switches are applicable in industrial, distribution of electrical power, etc. High voltage type isolation switches are utilized in substations for permitting isolation of equipment like transformers, circuit breakers. Usually, the disconnector switch is not proposed for circuit control but it is for isolation. Isolators are activated either automatically or manually. This article discusses an overview of what is an electrical isolator, its types, and its applications.

What is Electrical Isolator?

The isolator can be defined as; it is one type of mechanical switch used to isolate a fraction of the electrical circuit when it is required. Isolator switches are used for opening an electrical circuit in the no-load condition. It is not proposed to be opened while current flows through the line. Generally, these are employed on circuit breaker both the ends thus the circuit breaker repair can be done easily without any risk.


Electrical Isolator is used to separate any type of electrical component from the system while the system is offline/ online. Isolator doesn’t include any kind of system for avoiding arching throughout disconnection. As in an electrical substation, an electrical isolator switch is mainly used for disconnecting a power transformer once it is in a no-load situation otherwise a little load is there. In full load condition, isolators don’t operate.

Working Principle

An electric isolator working principle is extremely easy as it operates in different ways like manually operated, semi-automatic, and fully-automatic. Sometimes, these are used like switches so-known as electrical isolator switches. This switch can be opened or closed depending on the necessity. However, several times, these are arranged in a fixed position permanently to maintain isolation like transformers, in electrical transmission lines, grid stations.

An electrical isolator switch is one kind of device used to isolate a specific circuit by maintaining as well as preventing flowing currents. These switches are used in electrical appliances like kitchen tools, power grids, etc. Isolator switches are available in different types like a single-pole, double-pole, 3-pole, 4-pole, fused, and battery isolator switches.

Operation of Electrical Isolator

When there is no arc quench method is offered in the electrical isolator, it should be worked once there is no possibility of current flow throughout the circuit. So, no live circuit must be open otherwise closed through the isolator process.

A complete live closed-circuit should not be opened through the isolator process & also a live circuit should not be closed as well as completed through the isolator process to keep away from huge arcing among isolator contacts. So, this is the reason isolators should be open once the circuit breaker is open. Similarly, the isolator must be closed once the circuit breaker is before closed.

The operation of an isolator can be done through hand locally & using mechanical mechanism from a remote location. The arrangement of motorized operation is expensive as compared with hand operation; therefore choice must be taken before selecting an electrical isolator for the system which operates manually or mechanically is best for the system.

FCMA Soft Starter


FCMA Soft Starter

FCMA Soft Starter means Flux Compensating Magnetic Amplifier

In case of motor driven pumps, while starting, the motor normally takes 6 or 7 times full load current when started Directly on Line (DOL). Such high values of current have following implications.

a) Weakening of insulation and affecting motor life adversely.
b) Sudden jerks on incoming line, resulting into large voltage dips, which affect the other sensitive equipment operating on the same line.
c) High size of transformer / Generator, as a backup supply system.
d) Large jerks on the pumps and associated piping etc.


To eliminate these harmful effects, Soft Starters are used which reduce the starting current considerably and allow the motor to accelerate gradually.

The Soft starters provide gradual increase in voltage up to rated voltage ensuring even acceleration.

Benefits of Soft Starters

The provision of Soft Starters ensures following benefits.

a) Smooth starting by gradual acceleration of the drive system, thus preventing jerks and extending life of system components.

b) Reduction in starting current preventing mechanical, electrical & thermal weakening of electrical equipment such as motors, cables, transformers and switchgears.
c) Enhancement of motor starting duty by reducing temperature rise in stator winding and supply transformer, (subject to thermal curves).
d) Increase in Circuit breaker as well as contactor life.

To summarize, Soft Starters can optimize the starting performance of motors and motor manufacture can concentrate on improving running performance to ensure lower life cycle costing.

Types of Soft Starters

Various reduced voltage starting options have been available. The prominent among them are Star delta, Auto transformer, Electronics (Thyristors) and Flux Compensated Magnetic Amplifiers (FCMA) for LT motors. For HT motors predominantly FCMA Soft Starters are employed.

“Innovative Technomics Pvt. Ltd. (a Company situated at Pune, India) has developed very innovative FCMA Soft Starters to cover a wide motor KW range from 0.5 KW to 20,000 KW and supply voltage range from 220 V to 13400 volts.

These Soft Starters work on “Flux Compensated Magnetic Amplifier “ basis, (FCMA). This is innovative technology for incremental motor voltage & torque at constant reduced current. This technology has received wide global acceptance & many FCMA Soft Starters are operating satisfactorily in India & Abroad. In fact the largest Soft Starter for 10500 KW / 11KV motor is supplied for process compressor application in India and a 20000KW/11 KV soft starter is under manufacture. An aggregate of approx. 150,000 KW pump motors are provided with FCMA soft starters, in large pumping schemes in India and abroad.

Principle of Operation
FCMA Soft Starters are step less reduced voltage starters, which provide a constant low starting current with incremental voltage & torque characteristics to accelerate the motor & pump from stand still to full speed smoothly without any jerks.

The FCMA is connected in series with the motor either on the line or neutral side, so that the starting current is limited to a low value. The motor starts smoothly with the reduced current & the reduced torque. As the motor speed increases the impedance of FCMA reduces steplessly to keep the current constant and increase the motor torque so that the load is accelerated.


Theory of Flux Compensated Magnetic Amplifier (FCMA) :
The FCMA works on the principle of superimposition of sinusoidal fluxes on a common magnetic core where the net flux is the vector sum of the two components.

As the net flux is sinusoidal the FCMA does not generate any harmonics. The motor current is kept constant due to the balancing effect of Cemf feedback. If the motor current tends to increase the main winding flux will increase thus increasing the total flux & increasing the FCMA impedance & reducing the current to the original value. The FCMA is thus primarily a constant current controller & naturally provides current limiting action during the acceleration.
Note – It is important to note that FCMA is entirely different from Conventional magnetic amplifier. The conventional magnetic amplifiers (saturable core reactors) generate high harmonics content due to saturation & DC injection. FCMA is different and in fact, FCMA is zero Harmonics equipment. This aspect is thoroughly tested and certified while testing in India and Europe. FCMA is totally non-saturable and hence does not generate any harmonics.

BYPASS DEVICE
The bypass device bypasses the FCMA current controller in the run mode operation. Thus for continuous running of the motor no current passes through the FCMA & the motor gets full voltage. The bypass device essentially is a star contactor operated by fast closing & slow release D.C. magnet. The D.C. supply for operating the magnet is generated internally in the Soft Starter control scheme. The bypass device is designed for bypass duty i.e. to provide an alternative path to an already established current path in the FCMA thus preventing in any sparking during closing operation. The magnet is provided with a retentive core so that even in the event of control supply failure the magnet opens only after 0.5 to 1 sec, thus allowing the control scheme to trip the line side breaker. The bypass device thus is never subjected to current interruption duty & always opens on zero current. The contacts are hence not subjected to any wear & tear. An additional coil protection relay is provided for additional safety.

Salient Features of FCMA HT/LT Soft Starters

• Work on” Flux Compensated Magnetic Amplifier” basis.( FCMA).This is innovative technology for incremental motor voltage and torque at constant reduced current.
• Fully sinusoidal current and voltage waveforms without any harmonics and distortion.
• Starting currents normally adjustable from 2-4.5 times full load current, depending upon load and motor characteristics. The values of starting current can be adjusted at site and six such adjustments are provided.
• Built in RUN mode by pass contactor.
• Virtually no maintenance & can work in extreme ambient conditions.
• FCMA is natural air -cooled. No forced cooling required.
• Unique neutral side connection for high voltage units limits fault rating of soft starters and makes them very economical as well as very reliable .
• Can be retrofitted into existing systems without any major modifications. No special protections are required for soft starters. Conventional motor protections are sufficient.
• The general standards applicable are IS325/ IEC34 / BS4999 / BS5000


Unique advantages of FCMA Soft starters

• Smooth and step-less starting with very smooth by pass without any change over kick. Closed transition hence no momentary disconnection of supply.
• Amplitude control provides fully sinusoidal wave forms and hence totally harmonics free.
• FCMA has no moving parts and hence no wear and tear.
• No active electronic components and hence not prone to failure due to power supply spikes.
• High thermal withstand.
• No maintenance .
• Very reliable and user friendly. Easy to operate.
• Suitable for indoor/ outdoor installation depending upon requirements.
• FCMA assists optimisation of backup supply transformer/ generator. It can also optimize total power system.


Smooth Starting assisted by FCMA Soft Starter

A] Genset starting
Considerations – Engine step loading
Alternator KVA overload capacity
Alternator KVAR capacity
Soft starter advantages – Reduces torque hence power and Engine step load
Reduces KVA loading
Reduces KVAR loading and voltage drop
Result – User can optimize selection of Genset rating if motor is started with soft starter. This leads to large saving in Genset capacity and cost. Additionally the Genset will run at optimum load and efficiency, leading to fuel saving.


B] Transformer starting

Considerations – Transformer p.u. impedance
Transformer KVA overload capacity

Soft starter advantages – Reduces KVA loading
Reduces KVAR loading and voltage drop
Result – Customer can optimize selection of transformer rating if motor is started with soft starter. This leads to saving in transformer capacity and cost.

C] Starting of Motors on Limited Power Capacity
• Starting current limited to 2-3 times instead of 6 times as in DOL
• Voltage drop in transformers and Generators is limited to acceptable values
• Current load on transformers and generators is limited within safe limits
• Protection relays can be set for close protection Nuisance tripping during starting avoided

Conclusion : The application of FCMA Soft Starter with motor ensures optimisation of starting performance. Hence motor manufactures can ensure optimisation of starting & running performance with the help of FCMA Soft Starters & finally achieve lower life cycle costing.

Affination Process in Sugar Refinery with Material balance Calculation

Affination Process in Sugar Refinery with Material balance Calculation:-  In this article discussed about factors involved in affination process of standalone refinery with material balance calculation.

Material Balance of Affination Process in Sugar Refinery:-

What is Affination Process:-

Affination process is a first step in the sugar refinery process when high colored raw sugar taken as a input material. This process can be defined as washing and consists of removing the adhering film of molasses from the surface of the raw sugar crystal which is input raw material of sugar refinery.

In affination process involves mingling the input high colored raw sugar with affination liquor (Which is obtained in same process after centrifuged) and purging the mixture in centrifugal machine with hot water washing after the syrup has been spin off. After this process obtained two products named as affinated sugar and affination liquior.

The Affinated raw sugar directly taken to raw sugar melter and some required quantity of affinated liquor used for same process and remaining quantity sent to recovery house for massecuite boiling.

Operating Condition in Affination :-

Temperature of mingling affinated liquor

The purpose of the affination is to remove the sticky high colored molasses film. Hot mingling is best practice to reduce the viscosity and maintained around 70 to 75oC and magma temperature will be around 45 oC.

Parameters

Affination liquor brix                   72 to 74%

Affination liquor purity               75 to 85%

Affination liquor temperature   70 to 75 oC

Affination magma brix                90 to 92%

Wash water temperature           85 to 90 oC

Quantity of wash water             Depends upon required affination brix and colour of raw sugar.Examples of Solids and Purity Balance for affination of raw sugar in refined sugar process

Example – 1

Input parameters

 S.NO Description ValuesUOM
 1 Raw Suagr Quantity100T
 2 Raw sugar Brix 99.7%
 3 Raw Sugar Purity 98.8%
 4 Affinated liquor Brix 75%
 5 Affinated liquor Purity 85%
 6 Magma Brix 90%
 7 Affinated raw sugar brix 99.7%
 8 Affinated raw sugar purity 99.5%

Calculation:

Quantity of affination liquor  for magma preparation – 64.67 T

\frac{(Qty \ of \ raw \ sugar \ \ \times \ \ Raw \ sugar \ brix) \ - \ (Qty \ of \ raw \ sugar \ \ \times \ \ Magma \ brix)}{Brix \ of \ magma \ - Brix \ of \ \ affi. \ liquor }
Add caption

Hint : 

(((Quantity of raw sugar X raw sugar brix) – ( Qty of raw sugar  X magma brix))/ (Brix of magma – Brix of affination liquor)

Magma Quantity = 100 + 64.67 = 164.67 T

Purity of Magma = 93.38%

Hint: \frac{(Purity \ of \ raw \ sugar \ \times \ Qty \ of \ raw \ sugar ) \ - \ (Purity \ of \ affi. \ liquor \ \times \ Qty \ of \ affi. \ liquor \ )}{ Qty \ of \ magama}


Affi. Raw sugar99.58.38
Magma93.38
Affi. Liquor856.12
14.50


 S.NO Description Quantity SolidsUOM
 1 Affination Magma 164.7 148.2T
 2 Affinated Raw sugar 85.91 85.7T
 3 Affinated liquor 83.39 62.5T
 4 Wash water 4.64 0T
 5 Affinated liquor for magma preparation 64.7 48.5T
 6 Affinated liquor send to recovery house 18.73 14.04T

Example – 2

Input parameters

S.NO Description ValuesUOM
 1 Raw Sugar Quantity 100T
 2 Raw sugar Brix 99.7%
 3 Raw Sugar Purity 98.8%
 4 Affinated liquor Brix 75%
 5
 Affinated liquor Purity 80%
 6 Magma Brix 92%
 7 Affinated raw sugar brix 99.7%
 8 Affinated raw sugar purity 99.5%

Calculation:

Quantity of affination liquor  for magma preparation – 45.3 T

Hint : \frac{(Qty \ of \ raw \ sugar \ \ \times \ \ Raw \ sugar \ brix) \ - \ (Qty \ of \ raw \ sugar \ \ \times \ \ Magma \ brix)}{Brix \ of \ magma \ - Brix \ of \ \ affi. \ liquor }

(((Quantity of raw sugar X raw sugar brix) – ( Qty of raw sugar  X magma brix))/ (Brix of magma – Brix of affination liquor)

Magma Quantity = 100 + 45.3 = 145.3 T

Purity of Magma = 92.24%

Hint: \frac{(Purity \ of \ raw \ sugar \ \times \ Qty \ of \ raw \ sugar ) \ - \ (Purity \ of \ affi. \ liquor \ \times \ Qty \ of \ affi. \ liquor \ )}{ Qty \ of \ magama}

Affi. Raw sugar99.512.94
Magma92.94
Affi. Liquor806.56
19.50


 S.NO Description Quantity SolidsUOM
 1 Affination Magma 145.3 133.671T
 2 Affinated Raw sugar 88.96 88.7T
 3 Affinated liquor 59.96 45.0T
 4 Wash water 3.63T
 5 Affinated liquor for magma preparation 45.3 33.9706T
 6 Affinated liquor send to recovery house 14.67 11.00T

Conclusion : From the above examples, The quantity of solids are sent to recovery house will be reduced while maintaining the proper brix of magma and control the purity of affination liquor as much as possible.

If the quantity of solids of send to recovery house from affination process will be increased then massecuite % and final molasses percent is also increased.

Colour reduction in this process will be obtained around 50 to 60% on input raw sugar color. Some times more percent reduction required for input raw sugar colour having higher side. For this we go for more washing in centrifugal section and at the same time losses also will be increased.


Principles of Electromechanical Energy Conversion

Principles of Electromechanical Energy Conversion:-

• Electromechanical Energy Conversion :- Conversion of other forms of energy in electrical form have many advantages like easy control, utilise, reliable, efficient etc. An electromechanical energy conversion device is one which converts electrical energy into mechanical energy and vice- versa.

Categories of various electromechanical energy conversion: -

(i) First category:- involves small motion, processes only low energy signals from electrical to mechanical or vice-versa. Example : telephone receivers, loud-speakers, microphone.

(ii) Second category:- consists of force or torque-producing devices with limited mechanical motion. Example: electromagnets, relays, moving-iron instruments.

(iii) Third category:- consists of continuous energy conversion devices. Example: generators and motors.

State electromechanical energy conversion. Also explain its significance:-

"Energy can neither be created nor be destroyed". One can only change its forms using appropriate energy conversion processes Energy conversion takes place between well known pairs of forms of energy.

1. Electrical- Chemical

2. Electrical -Thermal

3. Electrical- Optical

4. Electrical - Sound

5. Electrical- Mechanical

Electromechanical energy conversion is a process in which electrical energy is converted into mechanical energy or mechanical energy into electrical energy. The main advantage of the conversion is that energy in electrical form can be transmitted, utilized and controlled more reliably, easily and efficiently. Energy conversion derives are required at path ends of an electrical system, since energy is neither available and nor required in electrical form. Electromechanical energy conversion finds application in following categories of system:

(a) Transducers: Devices for obtaining signal for measurement/control.

(b) Force-producing devices : Solenoid-actuators, relays, electromagnets.

(c) Devices for continuous-energy conversion : Motor/generator.

Principle of Electromechanical Energy Conversion in rotating machines : - 

When energy is converted from one form to another, the principle of conversion of energy can be evoked. According to this principle, energy can neither be created nor destroyed, it can merely be converted from one form to another. In an energy conversion device, out of the total input energy, some energy is converted into the required form, some energy is stored and the rest is dissipated. In view of this, the energy balance equation must include these energy terms, and for a motor, it is:

(Total Electrical Energy Input) = (Mechanical Energy Output) + (Total Energy Stored) + (Total Energy Dissipated)

For generator action,

(Total Mechanical Energy Input) = (Electrical Energy Output) + (Total Energy Stored) + (Total Energy Dissipated)

So, the principle of en rgy conversion is based on energy balance. For a rotating machine

W elec. = W mech. - W fld.

Where,

W elect. → net electrical energy input

Wmech→ energy converted into mechanical form

Wfld.→ stored energy + energy losses (change in magnetic stored energy).


Add caption

What is the definition of "PLC"?

What is PLC ?

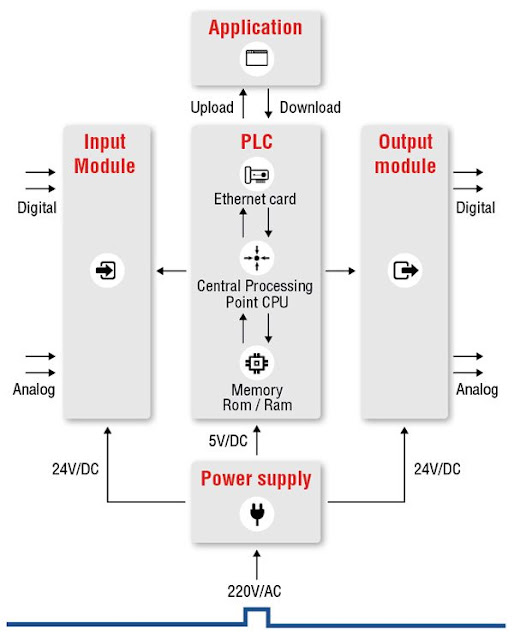
Programmable Logic Controller (PLC) focuses on automating different electro-mechanical processes taking place in various industries. With a well-programmed microprocessor, It has specially designed and implemented controllers which are immune to extremely high and low temperatures, humidity, dust, etc.

Just like any usual program, the coding is programmed on a computer. From here it is transferred to the PLC using a cable. After downloading the programs, these are loaded and stored in the PLC. In order to make sure the programs do not vanish at the time of power cut or switch off, it uses non-volatile memory storage.

It is programmed using a programming language called Ladder Logic. It is already known that it is an industrial computer. In order to program it, a programming language had to be designed in such a way, that the electricians and electrical engineer in an industry could easily understand and feel comfortable enough to code in it.

A Programmable Logic Controller consists of various input and output terminals. Using the input terminals, it interprets the logical states from switches and sensors. There are two logical states also known as high(or 1) and low(or 0). The output from the output terminals is used as a signal for various devices, providing them on/off controls. The electrical engineers understand the ladder logic diagrams and so it was the inspiration behind the programming language used to program its.

The most commons areas of use are in a washing machine, elevators and also traffic signals.

Definition:-

Programmable Logic Controller, more popularly known as PLC is a digital computer without a mouse or a keyboard or a monitor.

                                                            Or

A Programmable Logic Controller, or PLC, is a ruggedized computer used for industrial automation. These controllers can automate a specific process, machine function, or even an entire production line


Understanding PLC:-

Programmable Logic Controller is a small computer which automatically controls various processes and components in an industrial system. For the sake of comparison, let’s take a process that is manual as an example thinks of PLC as a brain controlling a finger on a trigger of an applicator. The brain sends a signal to the finger directing it to pull the finger when something is dispensed and when the brain wants to stop it sends another signal. Like most of the brains, it can multitask and it’s lightning fast Just like that, it can control much input and output signal like direct a paint line to change colors so all the widgets being painted go from one color to other.

Working:-

It communicates to the CPU status of the field devices as well as acts as a tool to control. The programming device is actually a computer loaded with programming software which will allow a user to create and make changes in the PLC software. The memory provides storage media for the PLC program as well as for other data.

How does a PLC work?

The PLC receives information from connected sensors or input devices, processes the data, and triggers outputs based on pre-programmed parameters.
Depending on the inputs and outputs, a PLC can monitor and record run-time data such as machine productivity or operating temperature, automatically start and stop processes, generate alarms if a machine malfunctions, and more. Programmable Logic Controllers are a flexible and robust control solution, adaptable to almost any application.

 There are a few key features that set PLCs apart from industrial PCs, microcontrollers, and other industrial control solutions:

• I/O – The PLC’s CPU stores and processes program data, but input and output modules connect the PLC to the rest of the machine; these I/O modules are what provide information to the CPU and trigger specific results. I/O can be either analog or digital; input devices might include sensors, switches, and meters, while outputs might include relays, lights, valves, and drives. Users can mix and match a PLC’s I/O in order to get the right configuration for their application.


• Communications – In addition to input and output devices, a PLC might also need to connect with other kinds of systems; for example, users might want to export application data recorded by the PLC to a supervisory control and data acquisition (SCADA) system, which monitors multiple connected devices. PLCs offer a range of ports and communication protocols to ensure that the PLC can communicate with these other systems.


• HMI – In order to interact with the PLC in real time, users need an HMI, or Human Machine Interface. These operator interfaces can be simple displays, with a text-readout and keypad, or large touchscreen panels more similar to consumer electronics, but either way, they enable users to review and input information to the PLC in real time.

Advantages:-

  • Easily programmable
  • Well shielded to outlast harsh situations
  • Input and output interface available where thousands of input and output can be controlled through a single PLC
  • Highly reliable
  • Easy to maintain

Required skills:-

PLC professionals are experts in concepts, electrical designs. They are also knowledgeable about fabrication and circuit board layout.

Also, they entail meeting with global standards in providing solutions to companies. This ensures making tasks easier by correct relaying of messages and the required team coordination.

Why should we use PLC?

The most common use of it is in washing machines, controlling traffic signals, elevators, etc. Also, we cannot neglect the use of PLCs in industries to monitor and control building systems and production processes.

Why do we need PLC and What can you do with PLC?

It is needed to automate machines in the industry so that human efforts can be reduced thus minimizing the human errors that might occur in the process. Consider a situation where a human handling a system missed to switched the motor on. Imagine the delay it might cause in the operation to begin. The simple solution to solve this is by automating the motor using PLC. So the basic and most important use of it is in the automation of machines.

Who is the right Audience for learning PLC Technologies?

The one-step solution to learning is various available courses online. It is also the best economical and easy way, however, the challenge in learning PLC online is you might learn the names and functioning of software and hardware parts of PLC, the ladder logic diagrams creation or configuring the various modules but just the theoretical knowledge is not enough. In order to be successful, one needs to have a hands-on experience. The one with an interest and background in logic diagrams and controls can start with the PLC programming tool. An elaborate program for an application is not at all an easy task to create. You need a lot of practice and hands-on to do so. In order to excel in this, one can begin from a small machine building company to gain insight and full-fledged skills and experience of the job.

Scope and How this Technology will help you in Career Growth?

As we all know that every industry is moving on to automating its processes and tools, the demand for the programmer is rapidly increasing. Industrial sectors in India like food and beverages, manufacturing industry, oil and gas industry, transport, process industries, etc are also stepping into Industrial Automation. As a matter of fact, technologies like AI, IOT are merging with OT or operational technologies which includes PLC, SCADA, DCS. Renowned companies like SIEMENS, Mitsubishi, Fanuc, Honeywell, etc provide their product and services all over the world. One can find many opportunities in IT and OT sectors as developer, testers, an analyst for it and so we can say that there awaits a bright successful future in automation for the same.

Conclusion

 These applications are specifically highly customized systems. It is cheaper when compared to the price of a specific custom-built controller. Generally, it requires less maintenance and is more robust, henceforth making the things they control work better, despite the environment.


V Curve of a Synchronous Motor:-

V Curve of a Synchronous Motor:- 


                                V curve is a plot of the stator current versus field current for different constant loads. The Graph plotted between the armature current Ia and field current If at no load the curve is obtained known as V Curve. Since the shape of these curves is similar to the letter “V”, thus they are called V curve of synchronous motor.

The power factor of the synchronous motor can be controlled by varying the field current If. As we know that the armature current Ia changes with the change in the field current If. Let us assume that the motor is running at NO load. If the field current is increased from this small value, the armature current Ia decreases until the armature current becomes minimum. At this minimum point, the motor is operating at unity power factor. The motor operates at lagging power factor until it reaches up to this point of operation.

If now, the field current is increased further, the armature current increases and the motor start operating as a leading power factor. The graph drawn between armature current and field current is known as V curve. If this procedure is repeated for various increased loads, a family of curves is obtained.

The V curves of a synchronous motor are shown below.


The point at which the unity power factor occurs is at the point where the armature current is minimum. The curve connecting the lowest points of all the V curves for various power levels is called the Unity Power Factor Compounding Curve. The compounding curves for 0.8 power factor lagging and 0.8 power factor leading are shown in the figure above by a red dotted line.

The loci of constant power factor points on the V curves are called Compounding Curves. It shows the manner in which the field current should be varied in order to maintain constant power factor under changing load. Points on the right and left of the unity power factor corresponds to the over excitation and leading current and under excitation and lagging current respectively.

The V curves are useful in adjusting the field current. Increasing the field current If beyond the level for minimum armature current results in leading power factor. Similarly decreasing the field current below the minimum armature current result results in lagging power factor. It is seen that the field current for unity power factor at full load is more than the field current for unity power factor at no load.

The figure below shows the graph between power factor and field current at the different loads.


It is clear from the above figure that, if the synchronous motor at full load is operating at unity power factor, then removal of the shaft load causes the motor to operate at a leading power factor.

Effect of Temperature On Resistance | Resistance Temperature Coefficient

Effect of Temperature On Resistance | Resistance Temperature Coefficient Fundamental of Electrical Engineering | Effect of Temperature On Re...